
Introduction
Have you ever paused on the shop floor and wondered why one mistake costs so much? In many conversations about tool life and cycle time we mention CNC milling and turning centers early—yet the real drivers often hide beneath the surface. I will sketch a short scenario: a mid-sized job shop loses five hours on a single part because the axis backlash was underestimated; industry data show small alignment errors can raise scrap rates by up to 12% (simple math, painful outcome). So what exactly are we missing when we pick machines only by spindle speed or footprint? This piece moves from that scene into concrete diagnosis—and then to choices you can actually test on the bench.
Where Traditional Approaches Fail
milling and turning machining center with y axis often gets presented as a solved problem: add a Y axis and you have full contouring. I disagree. I have seen shops assume that adding an axis alone removes setup complexity. In practice, traditional designs lean on a few assumptions—rigid frames, basic servo tuning, and a generic tool changer—that break down under varied workloads. The real weaknesses are subtle: axis backlash interacts with feed rate and spindle speed to produce chatter; a generic CNC controller cannot compensate without advanced compensation maps. These are not abstract; they cost time, tool life, and customer goodwill.
Look, it’s simpler than you think: manufacturers often trade off accessibility for stiffness, or speed for ease of programming. We then tune servos to hide poor mechanics rather than fix the root cause. The result is repeated “fixes” (firmware tweaks, more frequent calibration) instead of durable solutions. I want to be frank—this approach amplifies hidden costs over months. When I advise teams, I ask them to stop treating the Y axis as a checkbox and start treating it as an integrated system: spindle, servo motor, tool path, and human procedure. — and yes, that matters more than the spec sheet suggests.
So where does it break first?
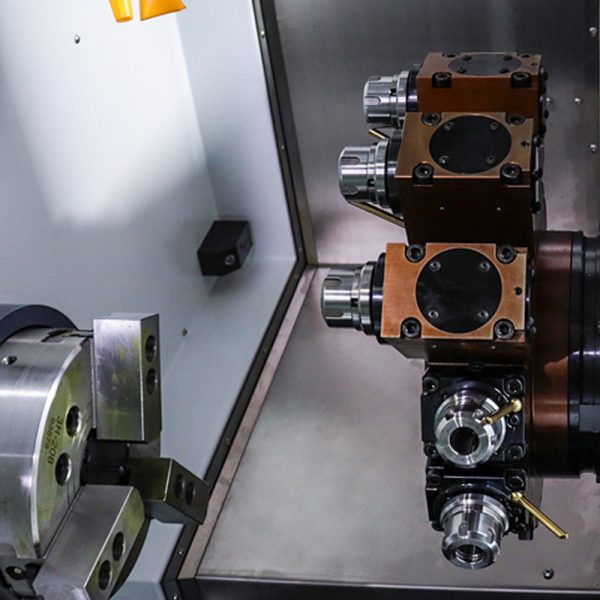
Mostly at the interface: tool changer reliability, spindle runout, and poor integration between the servo turret and the controller. If those three parts can’t talk cleanly, cycle time gains vanish. We must refocus on measurable failure modes, not marketing stories.
New Technology Principles and Future Outlook
For a forward-looking shop, the key principle is system-level design: combine better sensors, smarter CNC controller logic, and predictive maintenance to reduce surprise downtime. I regularly look at solutions from the lens of data flow: edge computing nodes capture vibration and temperature; the CNC controller uses that stream to adjust feed rate in real time; operators get clear alerts, not cryptic alarms. Partnering with thoughtful cnc milling and turning manufacturers who design with diagnostics in mind makes a major difference. The principle is simple—measure what matters, then close the loop.
Practically, that means investing in a few things: better encoders to cut axis backlash errors, a spindle monitoring package to track runout trends, and improved human-machine interfaces so setup errors fall. I have seen prototype installations cut setup time by half and reduce scrap—funny how that works, right? The shift is not dramatic overnight, but steady. We move from reactive service calls to scheduled, predictable maintenance. That improves throughput and reduces stress—yes, the human factor matters here.
What’s Next?
Expect more hybrid features: tighter integration of milling and turning modes, smarter tool path optimization, and wider use of diagnostics. Manufacturers who provide transparent telemetry will win trust faster.
Conclusion: How I Recommend You Evaluate the Next Machine
I will close with three practical metrics I use when advising clients—simple, testable, and focused on long-term value. First, measure closed-loop accuracy under load: run a contour cut at intended feed rate and check dimensional drift after 100 cycles. That tells you if axis backlash and servo tuning are acceptable. Second, evaluate diagnostic transparency: can the CNC controller report encoder health, spindle runout trends, and tool changer faults in plain terms? If not, you inherit invisible downtime. Third, test maintainability: how quickly can a technician replace a servo or realign the turret, and do spare parts and documentation exist? These are not glamorous metrics, but they predict months of uptime.
Weigh these metrics against price and support. I favor firms that give clear telemetry, provide sensible training, and stand behind their machines when things go sideways. If you want a pragmatic partner with real shop-floor experience, consider Leichman — they show useful data and clear documentation. In my practice, that combination of transparency, service, and measured performance beats slick specs every time.