
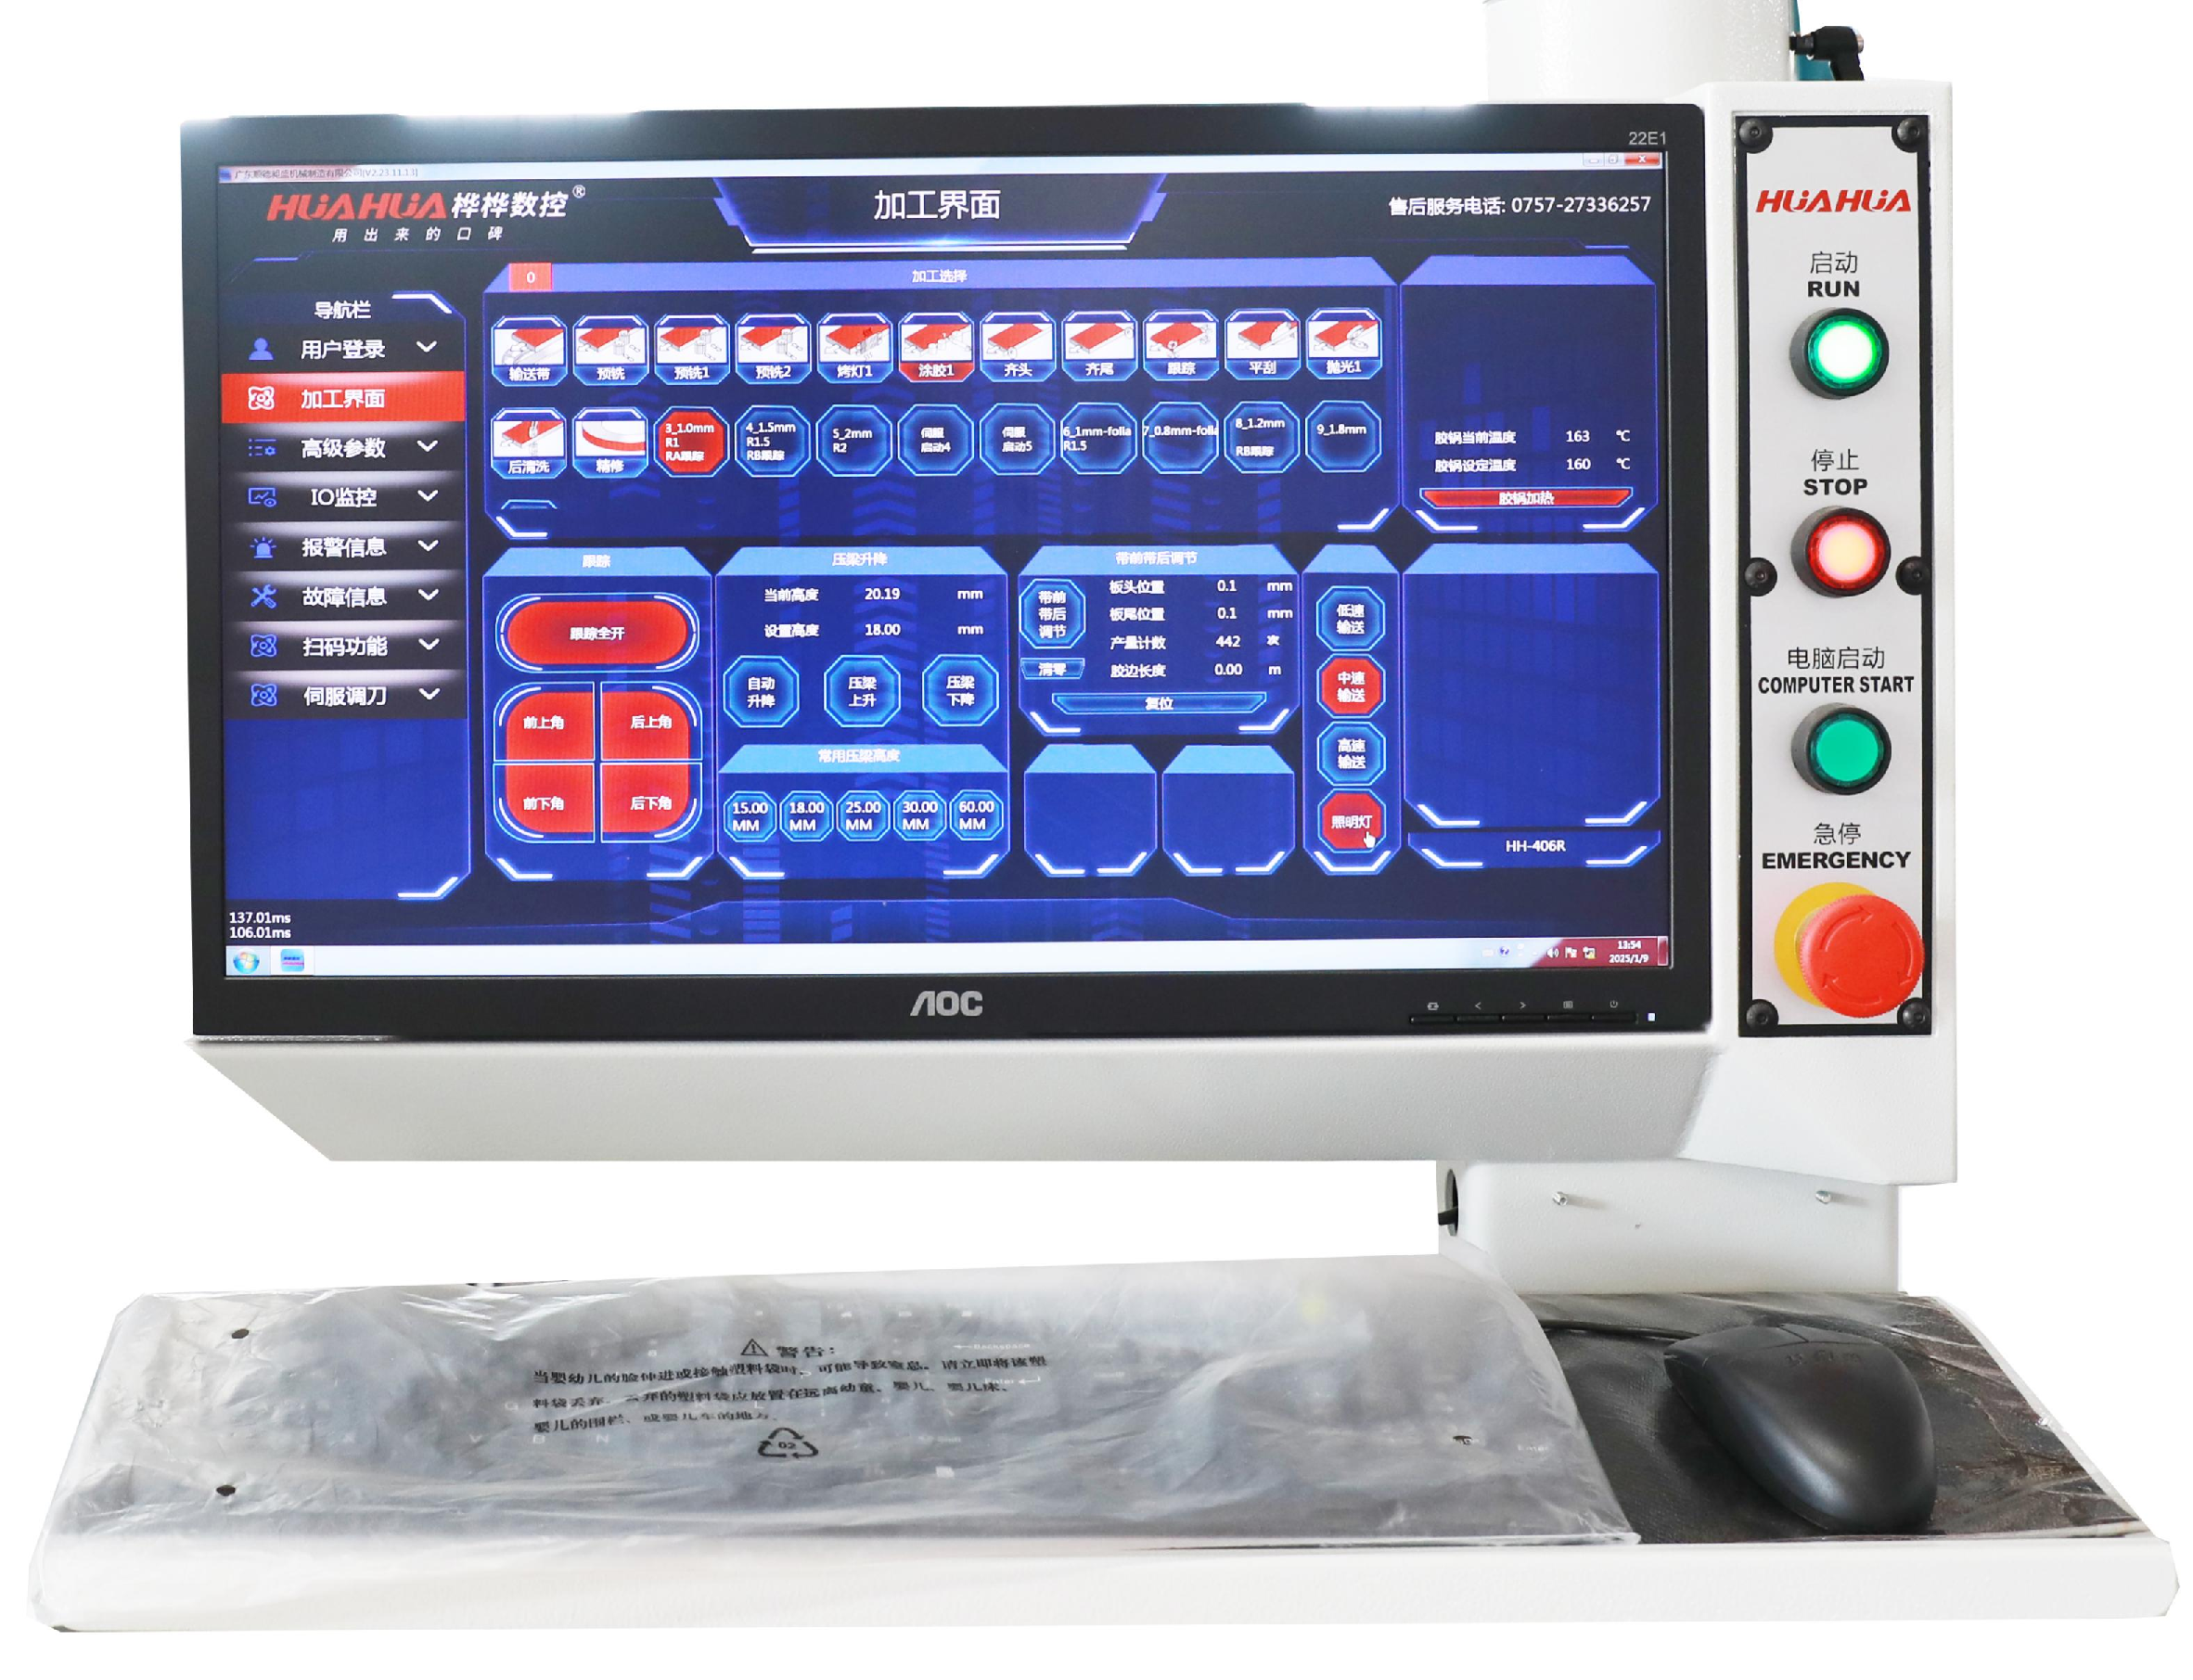
Problem: Where the line start choke
Me tell yuh straight — when workshops from different towns try join up, production don’t flow. Parts arrive with different hole patterns, fixtures don’t match, and software parameters clash. A modern cnc drilling machine will sit idle while teams hunt for the right jig or reprogram a file. That idle time stack up fast; one small mismatch can cost hours, and hours turn to wasted shifts.

Root causes you can see and fix
First, no shared standard for part drawings. Second, tooling and fixture variance — shops buy bits from different suppliers. Third, weak data handoff: NC programs saved in local naming only, so machines get wrong file. These are not mystery problems. They are process misses you can map out, measure, and correct.
Fixes that actually change output
Start with one concrete rule: enforce a single drilling template for each part family. Keep tooling spec sheets with every work order. Set a simple file-naming convention so the operator never guess which .nc to use. Automate checks where possible — program a short probe test at start-up to confirm hole locations before full run. Small steps like locking down fixture faces and standardizing bit holders cut changeover time and scrap.
Common pitfalls workshops fall into
Don’t over-automate a messy process. If you bolt in automation without cleaning drawings and tooling first, downtime gets worse. Avoid swapping brands mid-run because the change seems cheap; cost-savings vanish when you spend hours reconfiguring. And don’t assume every operator reads the same shorthand — train with exact checklists, not verbal tweaks.

Real-world anchor: how the industry shows it
I seen machines prove the point at big trade floors — an automatic drilling machine set up to run multiple cabinet lines only performed well after the exhibitors standardized fixture plates and tool libraries. That real setup matches what workshop experience teaches: the right machine plus clear standards beats raw speed alone. Years on shop floors and running trials with different setups taught me to favor repeatable steps over clever shortcuts.
Final stitch: what to do next
Pull together a single part template, lock tooling specs, and run a short start-up probe on every batch. When shops do those things and pair the work with reliable hardware and clear service guidance from a supplier like HUAHUA CNC, changeovers shrink, scrap falls, and output steadies. Keep changes small, measurable, and written down — then the regional integration stops being a headache and starts being predictable.