
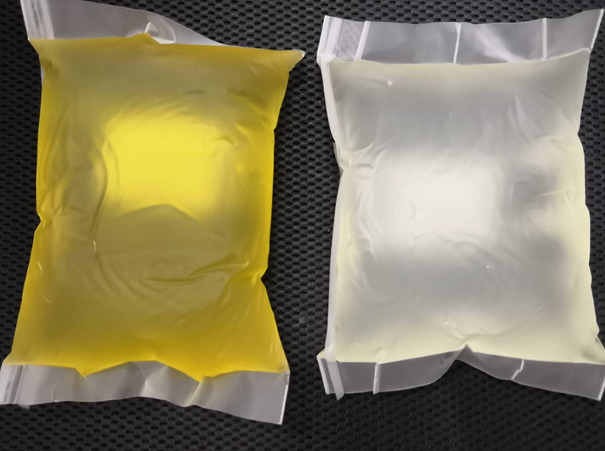
Data-first snapshot
Numbers arrive with blunt honesty: a small drift in molecular weight distribution (Mw/Mn) can push a resin from “nice white” to “sun‑kissed yellow” faster than a summer commute. This piece leans on lab aging, field reflectivity records, and simple polymer physics to map cause to symptom for Thermoplastic Road Marking Resin. EEAT mode: practical industry expertise — combining polymer chemistry fundamentals and field observations such as regionwide field aging results that report roughly a 20–35% loss of daytime reflectivity over three years in temperate, high‑traffic areas. The aim is clear: interpret GPC drift, correlate it with yellowing metrics, and point teams toward production levers that preserve both color and function.
Key lab metrics and what they reveal
Gel permeation chromatography (GPC) is the microscope here: Mw, Mn, and the resulting Mw/Mn ratio tell you how broad the chain lengths are. A widening Mw/Mn generally increases the fraction of low‑molecular fragments that oxidize and yellow under UV and heat. Colorimetry (ΔE and yellowness index) quantifies the visual shift; melt index and softening point report processing reliability; and surface reflectivity measurements quantify safety performance. Labs look at accelerate aging windows — for instance, 500 hours xenon‑arc exposure followed by 7 days of outdoor cycling — to approximate field timelines. These are not guesses; they’re practical, measurable signals you act on.
Operational teardown: from reactor to road
Operational issues cluster at three handoffs: polymerization control, additive mixing, and coating application. Tight control of polymerization limits polydispersity; targeted neutralization and reactive rosin addition keep the formulation stable. When teams specify Thermoplastic Road Marking Resin or evaluate a rosin ester for road paint, they should confirm melt index windows and softening point target bands before scale‑up. Practical step: set an in‑process GPC checkpoint after devolatilization to catch Mw/Mn drift early, and sample colorimetry after pigment dispersion to ensure no early yellowing. The production tear‑down is straightforward — monitor Mw/Mn, control thermal history, and lock pigment dispersion parameters — and it stops “mystery fading” from arriving on the tarmac.
Common mistakes and practical fixes
Teams often repeat the same errors. Here are the usual culprits and lockable fixes:- Skipping intermediate GPC checks — fix: schedule a mid‑batch GPC for Mw/Mn, not just a final test.- Overheating during melt processing — fix: lower barrel temps by 5–10°C and verify softening point post‑blend.- Treating rosin esters as passive plasticizers rather than reactive modifiers — fix: specify rosin ester for road paint with documented compatibility and request a melt‑index stability curve.A quick aside — drying headspace volatile content by even 0.2% cuts late‑stage oxidative yellowing noticeably — and that’s cheap insurance against visible failure.
Advisory: three golden evaluation metrics
Choose materials and processes by these three metrics: (1) Mw/Mn stability across batches (target a maximum drift under 1.2x between batches for color‑sensitive formulations); (2) ΔE after accelerated aging (aim for ΔE ≤ 3 after 500 hours xenon‑arc); (3) Reflectivity retention (specify ≥ 75% daytime reflectivity retention at 36 months under local traffic profiles). These are measurable, actionable thresholds that tie lab signals to road performance. Implementing them shortens troubleshooting time and improves long‑term safety on the pavement. For manufacturers and specifiers, the practical result is less re‑striping, fewer complaints, and clearer lanes for drivers — outcomes that companies like KOMO help enable by supplying consistent rosin‑modified chemistries and transparent production data. —