
Opening Scene, Real Numbers, One Big Question
Picture a late-night sample check. The team is tired, the launch clock is loud, and a tiny cap wobble derails the plan. Your cosmetic packaging manufacturer promises a smooth path. Working with cosmetics packaging manufacturers sounds simple, but small details rule the day (and night). Industry data shows that packaging drives a large slice of launch risk; some audits put 30–40% of delays down to fit, finish, or test failure. Returns also spike when pumps leak or threads strip—quiet issues in the lab, loud ones in the store. So, why do smart teams still get caught?
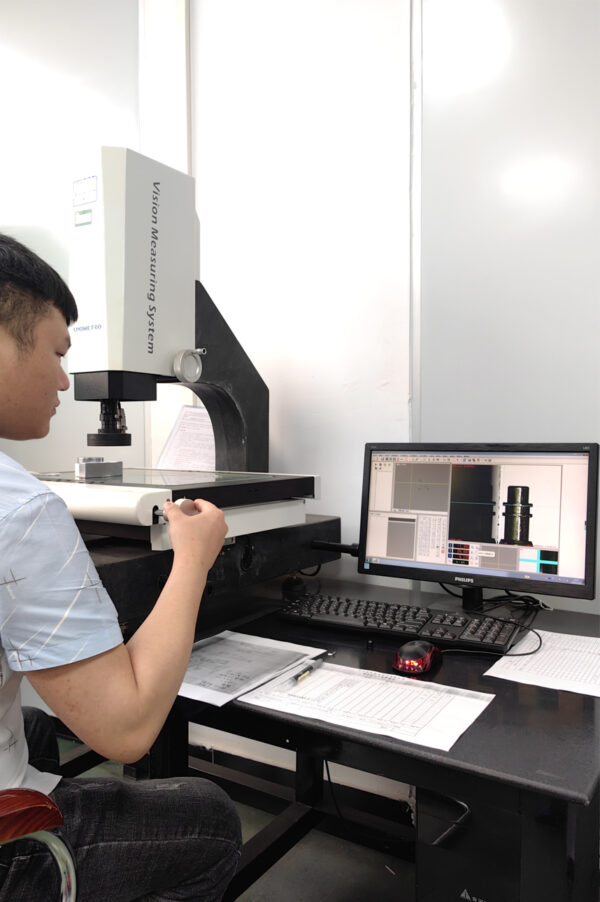
In this field, precision hides in plain sight. Color match shifts when line heat drifts. Anodizing on metal collars changes with bath age. Vacuum metallization can bloom if the basecoat is off. MOQ pressure squeezes timelines, and ISO 22715 checks may arrive too late to help. The scenario is relatable, yes, but the data is clear. One gap leads to many. Shall we move from the story to the structure—so we can avoid the same trap next time?
The Hidden Fault Lines in the Usual Process
Why do good packs still fail in market use?
Here is the direct truth: the default process bakes in risk. Many cosmetics packaging manufacturers start with off‑the‑shelf molds. That cuts tooling cost, but it also locks thread pitch, wall thickness, and gate position. If your formula is viscous or volatile, an airless pump needs a tighter tolerance. Injection molding cannot fix that at the last step. Then the fit test gets rushed. Torque test data is taken in a cool lab, not a hot truck. Color approval happens on a chip, not a molded part. Look, it’s simpler than you think: you tested the wrong thing, in the wrong place, at the wrong time.
Another fault line sits in materials. PCR resin lots vary in melt flow. That shifts shrink, which changes cap grip. Barrier properties move when a liner spec changes by a hair. A gate vestige bumps the sealing plane by 0.1 mm, and now the leak rate creeps up. These are not dramatic errors. They are normal drift, amplified by tight calendars. The hidden pain point is context. Tools, resin, torque, and transport need one joined plan. When they are split across vendors, small misses stack—fast.
From Faults to Future: A Comparative View of What Changes First
What’s Next
Forward-looking plants manage drift, not just defects. Some cosmetic packaging manufacturers china now run closed-loop molding with cavity sensors. They watch melt temp and pressure in real time, then nudge machine settings before parts go out of spec. Inline vision checks catch short shots and flash. SPC charts track cap torque on the line, not only in the lab. It sounds technical, but the principle is simple: measure early, correct sooner—funny how that works, right? Add digital color targets at the press, and you cut shade calls by half. Add humidity-controlled storage for liners, and seal variance drops again.
The near future is also comparative. Old way: approve on golden samples, then pray. New way: approve on a digital twin plus pilot run, then lock with a control plan. Old way: test pumps with water. New way: test with your formula or a viscosity match. Plants that log resin lot, cavity ID, and torque data tie each SKU to a real history. That helps recalls and boosts trust. It also trims waste. A small case in point: when one line swapped to pre‑set capping with live torque feedback, complaint rates fell 28%, and rework time fell 22%. Not magic—just better signals at the right step.
How to Choose Wisely: Three Metrics That Tell the Truth
Here is a clear way to decide. First, ask for first-pass yield at pilot and at mass. Over 92% at pilot and stable at scale shows control across molding, assembly, and capping. Second, check torque capability on your closure system. A Cpk above 1.33 with your formula in the bottle points to real-world seal strength, not a lab-only win. Third, demand traceable PCR content and liner specs across lots, with a simple report you can read. If they cannot show stable melt flow and shrink, expect color and fit drift—then expect delays. Summed up: measure early, test with context, and choose partners who design for variance, not only for average. When teams do this, launches feel calm—and it saves time. For a steady reference point on these methods, see NAVI Packaging.