
Introduction
What happens when a single machine can shave hours off a job and free a skilled operator for higher-value work? I see that every week on the shop floor. CNC turn mill center manufacturers are getting more questions from shops about throughput, repeatability and long-term service. Recent shop-floor surveys show many shops report a 15–35% gap between promised cycle times and real output (yes, the difference matters). So: how do you cut through marketing and pick a machine that truly moves the needle for your business?
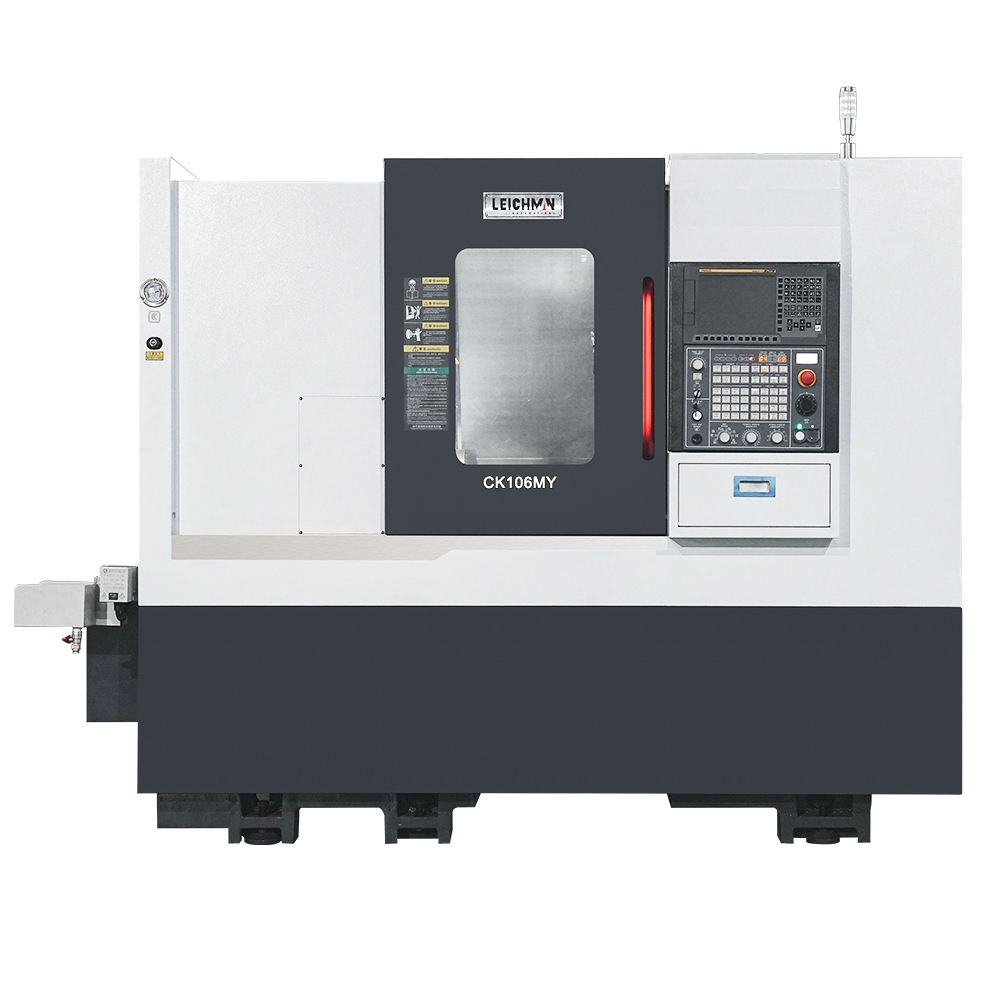
I’ll share what I watch for, what I reject, and why a few simple checks save you time and money. Short reads. Clear measures. Then we dig into the design problems that hide behind glossy specs.
Where traditional solutions let you down (cnc mill turn center)
cnc mill turn center promises combined lathe-and-mill capability in one envelope. On paper, that solves setup and handling issues. In practice, many legacy approaches still trip shops up. First, manufacturers often trade rigid axis control geometry for marketing claims about “universal” work envelopes. That sounds good until you run a family of parts that need tight spindle-to-tool repeatability. Second, suppliers under-spec servo motors and drive electronics to hit a price point. This reduces torque margin during heavy cuts and leads to chatter and scrap. Third, service networks are inconsistent: replacement power converters and spindles can take weeks to arrive (and by then the job is late). Look, it’s simpler than you think — those three failings explain most downtime.
Why do these issues persist?
One reason is historical design inertia. Engineers fix what the market demanded five years ago, not what users need today — edge computing nodes for diagnostics arrive late; tool turret indexing accuracy is still treated as optional. I find that many fault chains start small: a slightly loose turret fit, a marginal spindle preload, a software update that assumes perfect axis calibration. Each is fixable, but only if you surface them during evaluation and testing. — funny how that works, right?

Future outlook and comparative view: what to demand next
Looking ahead, I weigh two things: rugged baseline mechanics and intelligent sensing. A machine with honest mechanical stiffness, good spindle bearing preload, and the correct servo motor sizing will survive years of hard cuts. Atop that, I want smart diagnostics — vibration sensors, simple edge analytics, and clear alarms. These are not flashy extras. They let you spot tool wear, spindle imbalance, or coolant entrainment early, before scrap accumulates.
What’s Next?
Take the example of a shop that swapped a decade-old cell for a modern cnc multi axis turning milling center. They reduced setup by half and cut cycle time by 20% on complex parts. The gains came from matched axis control, a stiffer bed casting, and faster tool changes — not from a handful of extra features. My point: prioritize fundamentals, then add intelligence. The future favors machines that pair proven mechanics with smart feedback, not gadgets that sound good in a brochure.
Here are three evaluation metrics I use when I advise shops (practical, measurable): 1) Repeatability under load (microns), 2) Mean time to first failure for wear items (months), and 3) Availability of critical spares in your region (days). Use these with real cuts and real fixtures. You’ll avoid the shiny-box trap and pick a machine that pays back — and that’s what matters to me.
I’ve written this from hands-on experience. I’ll be blunt: specs lie unless you test them. Ask for cut trials. Push the spindle. Measure the finish. Talk to local service teams. If you need a starting point, look at suppliers who combine sound mechanics with clear support plans — that’s the path I recommend. For practical options and further details, check Leichman.