
Introduction
How many times have you watched a job run late into the night and wondered whether the next shift could do better? I ask because small changes on a line can add up — dramatically. CNC equipment manufacturers are staring at hard numbers: shops that adopt smarter controls report 20–40% higher uptime and faster cycle times in real cases (actual shop audits, not marketing slides). So where do we start: new controllers, smarter spindle tuning, or better tooling strategies?
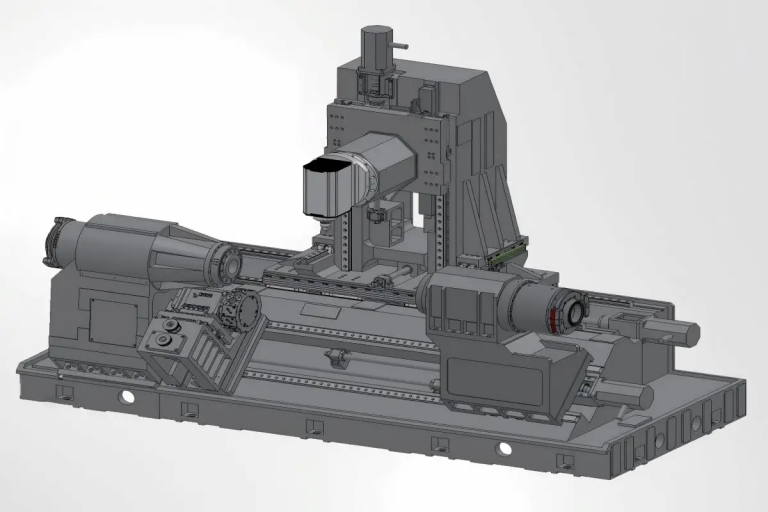
I want to be direct: this piece draws on shop-floor snapshots, controller logs, and my hands-on experience with retrofit projects. You’ll see terms like CNC controller and spindle motor used plainly, and I’ll point to practical gaps that trip teams up daily. We’ll move from problems to practical fixes, and then look ahead at what to weigh when choosing systems. Ready — let’s dig into what actually slows a line down and why that matters for capacity and margins.
Where Traditional Fixes Break Down
Start with a simple fact: a milling machine with cnc can only be as fast as its weakest link. I’ve watched lines invest in high-speed tooling but leave the old feed tables and outdated toolpath logic untouched. The result? Short bursts of speed and long stretches of idling. That mismatch shows up as chatter, missed tolerances, and extra manual checks. In technical terms, poor toolpath optimization combined with a lagging CNC controller and inconsistent feed rate settings causes far more scrap than anyone budgets for.
(Look, it’s simpler than you think.) We often assume more horsepower or a better spindle motor will fix throughput. It helps — but not if the toolpaths aren’t tuned for the part or if the tool offsets and compensation are wrong. I’ve seen shops chasing spindle RPM while ignoring thermal drift and workholding stability. The hidden pain here is time: setup time, inspection time, rework time. These are invisible costs that pile up into major losses. And yes — funny how that works, right?
So what’s really failing?
Short answer: coordination. The CNC stack needs synchronized tuning — controller parameters, toolpath strategy, coolant use, and workholding. Any weak link forces the rest to run below peak. We talk about edge computing nodes and power converters in theory; the reality on the floor is simpler: make the entire chain work together.
New Principles and Practical Choices
Looking forward, I favor two active approaches: clear measurement and targeted upgrades. Measure cycle stages. Pick the slowest few and fix them first. When you evaluate new hardware or software, think beyond peak spindle rpm. Ask whether the system improves toolpath planning, reduces idle time between operations, or automates setup checks. For many shops, adding modest digital tooling for tool-life tracking and basic toolpath optimization yields better gains than a full CNC replacement. In short: small, smart steps often beat big, blunt investments.
On the tech side, we should consider how sensors and simple analytics change choices. Sensors that monitor vibration and thermal drift can feed a controller that adapts feed rate on the fly. That reduces scrap and keeps tolerances tight. I also recommend looking at how your vendor links controller updates to real-world test parts, not just demo programs. Real validation matters. — I’ve learned this the hard way in retrofit projects, and so have several shops I advise.
What’s Next
Before you sign a big check, keep three evaluation metrics in mind: 1) measurable cycle-time reduction on real parts; 2) ease of integration with your existing CNC controller and tool management; 3) uptime gains after three months in production. These metrics force vendors to prove value in your environment, not just in a lab. I usually run a short pilot and insist on data collection during that pilot — if the vendor can’t show numbers, I walk away. That discipline separates sales talk from real results.
To sum up, improvements come from thoughtful fixes: better toolpath optimization, tuned feed rates, reliable workholding, and targeted sensor use. I’ve seen shops transform throughput without replacing every machine. If you want a partner with practical, measured steps, check out Leichman. We’ve done this work with teams who care about real gains, not just glossy specs.