
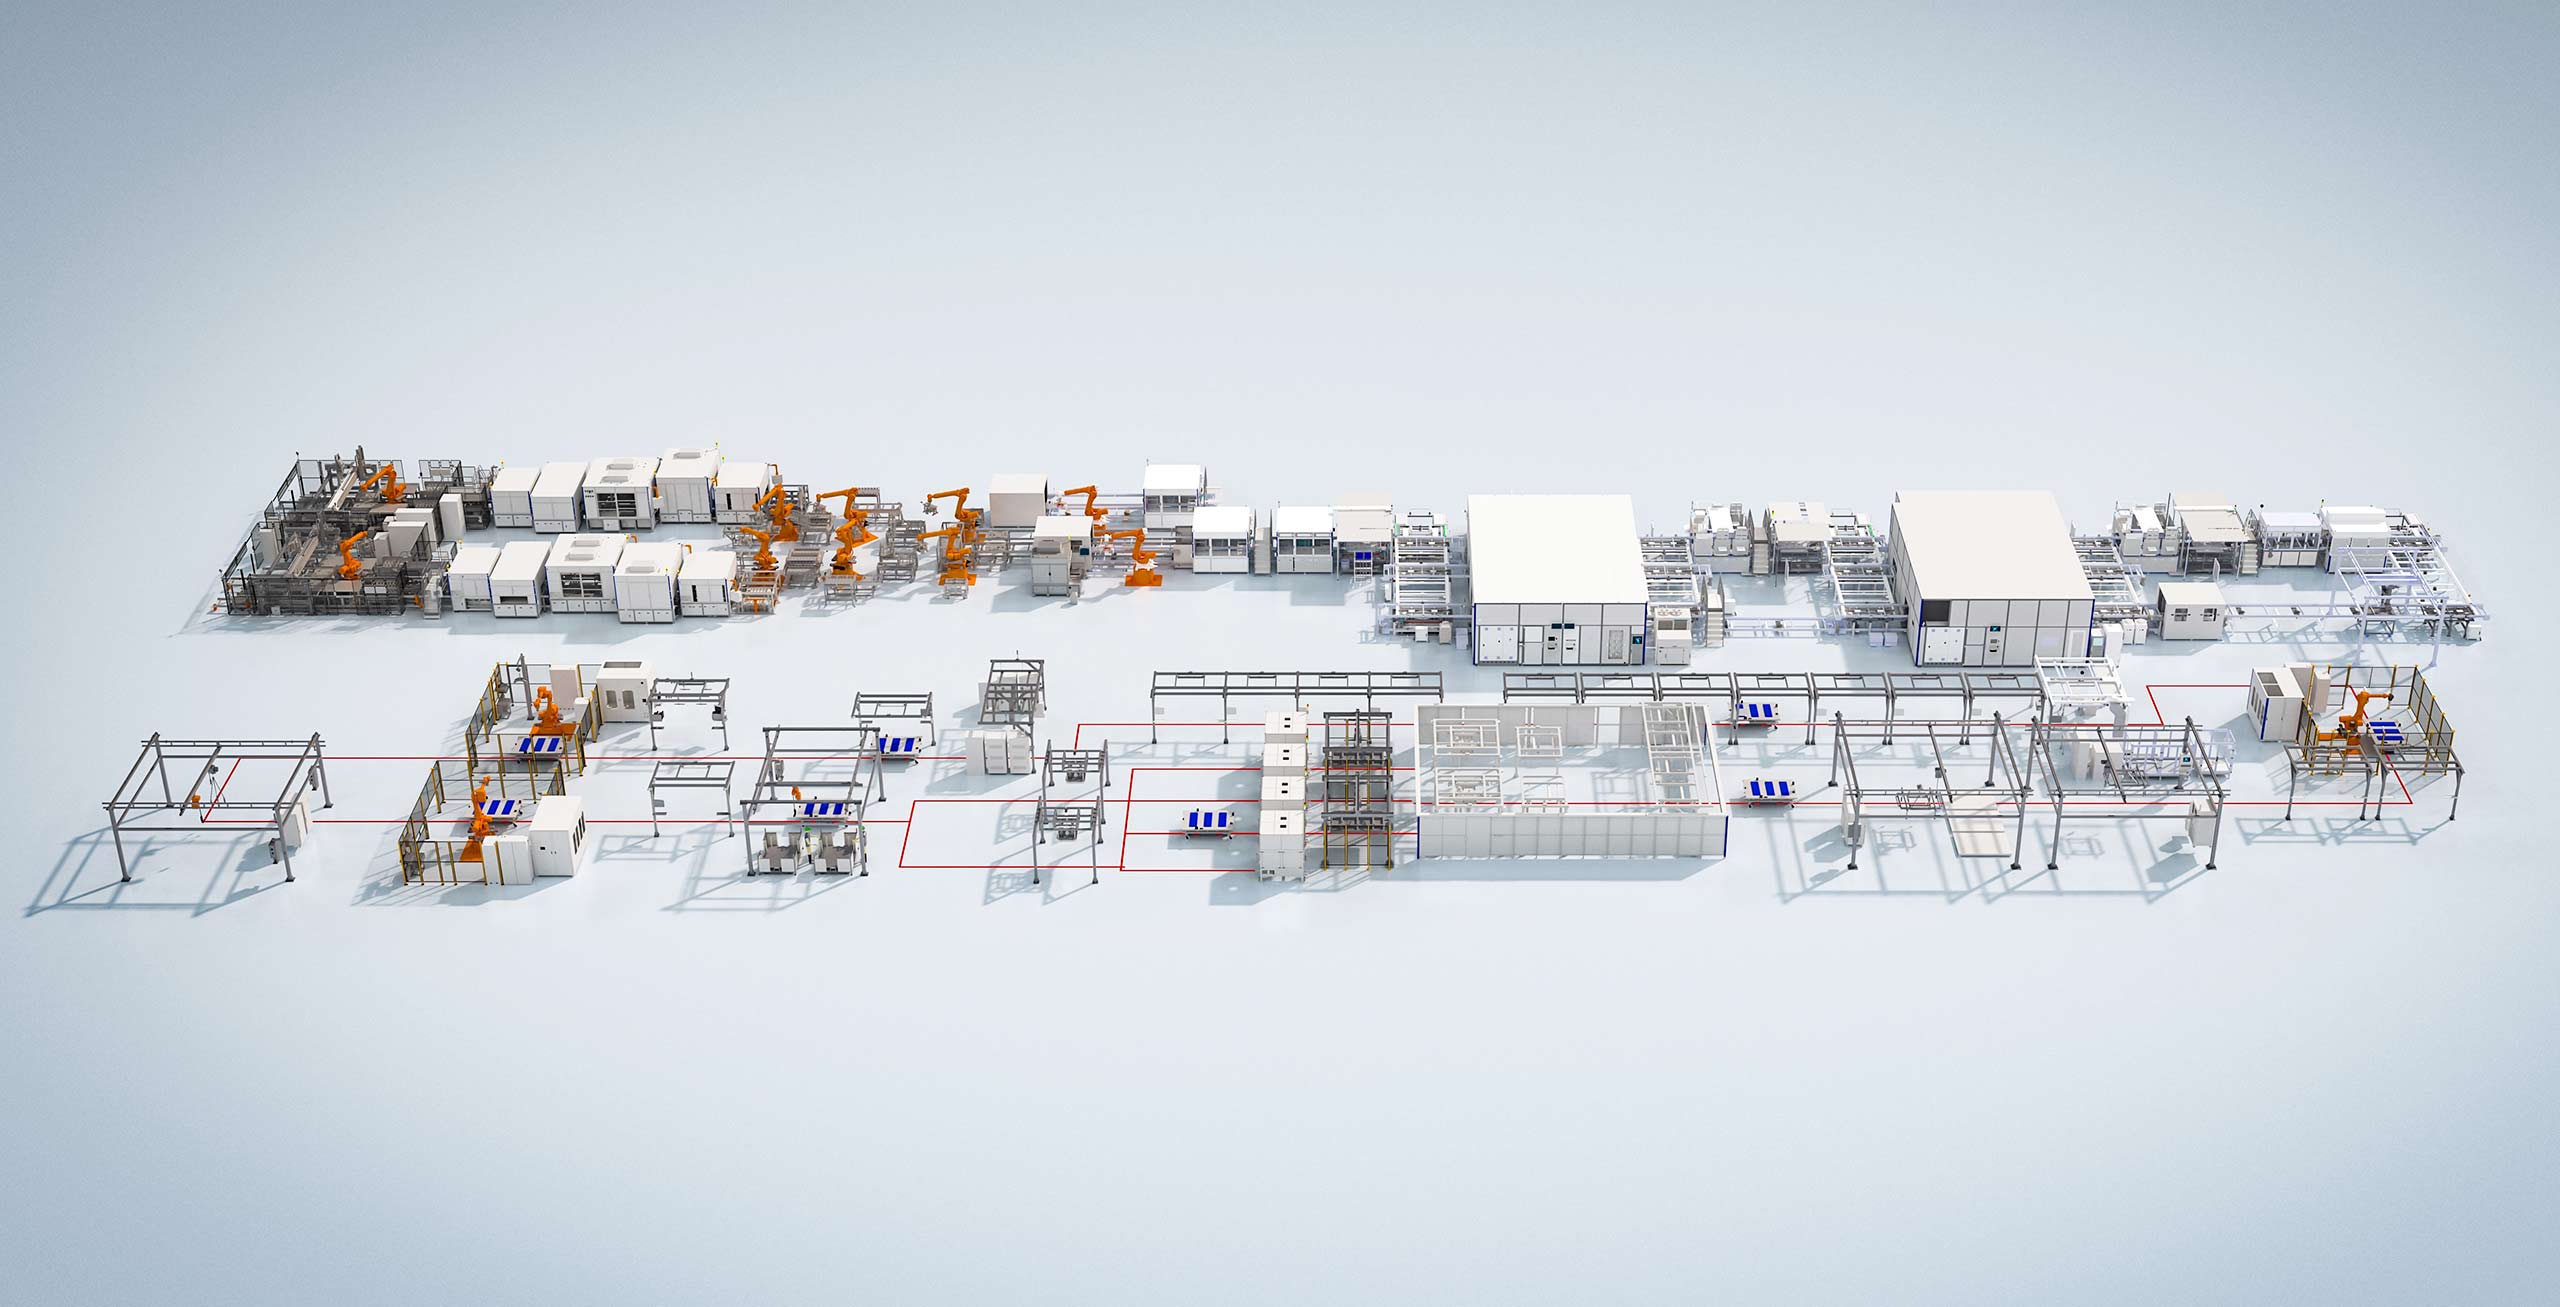
Why many CTP lines trip up before they start
Right then — most folk try to bolt machines together and hope for the best, and that’s where trouble begins. I’ve seen battery pack assembly suppliers shoved into cramped bays without thinking about throughput, and the whole line grinds to a halt. The problem’s simple: poor layout and mismatched capacity make faults more likely and fixes costlier. If you’re dealing with printed circuit pattern (CTP) production, you need to sort flow and capacity before you buy another conveyor.

Common failure modes that sneak up on teams
Problems tend to come in three flavours. First, bottlenecks: one process runs slower than the rest and queues pile up. Second, variability: cycle times wander and the line loses rhythm. Third, accessibility: maintenance can’t reach machines without stopping production. Those faults ruin yields and morale, and they’re easy to prevent if you spot them early.
Layout rules that actually prevent bottlenecks
Lay the shopfloor to match the slowest, most error-prone process. Think of the line as a river — you don’t try to shove a waterfall through a narrow sluice. Practical steps that work:
– Place inspection and error-prone stations where operators can intervene without cutting power.
– Reserve buffer space upstream of slow stations equal to at least one hour of peak production.
– Use modular cell layouts for parallelism rather than a single long line when processes vary in speed.
Capacity maths without the faff
Calculate required hourly capacity by working from demand back to machine hours. Don’t guess. Basic checks to run now:
– Determine target output per shift and convert to parts-per-minute.
– Measure actual cycle time (not vendor spec) for each process and add realistic downtime (planned + unplanned).
– If a station’s required uptime or speed exceeds its spec by more than 15%, plan a parallel cell or upgrade.
Process requirements that stop repeated fixes
Processes need clear inputs, outputs, and quality gates. A station that accepts variable input quality will always be a weak link. Insist on:
– Standardised input kits and jigs so machines face the same conditions every run.
– Inline inspection early, not after critical irreversible steps.
– Defined corrective action steps for common faults, written and practised.

Practical pitfall checklist — skip these at your peril
Here’s a quick list to run through with your team before committing to layout or kit purchases:
– Overreliance on vendor cycle times without shopfloor trials.
– No physical buffer space mapped in metres or minutes.
– Maintenance access requires full line shutdown.
– No plan for variability: single-point throughput assumptions.
– Ignoring upstream supplier quality issues that propagate defects.
How I proved this works — a real-world anchor
I’ve overseen line redesigns in the Shenzhen manufacturing hub where a simple rework of buffer allocations and maintenance access cut stoppages by a clear margin. That hands-on troubleshooting taught me to privilege physical flow and operator reach over fancy control panels.
Choosing equipment and integrating suppliers
Match machine capability to measured demand, not hoped-for figures. When you bring suppliers on board, set acceptance tests that reflect real cycle times and fault modes. If you need supplier options for power-hungry or high-density builds, consider the same partners you’d use for battery pack assembly suppliers that can demonstrate consistent output under shopfloor conditions.
Quick examples of layout fixes that deliver
Two small fixes that usually pay off fast:
– Move visual inspection upstream and add a two-minute buffer rack — this prevents rework at final test.
– Split an overloaded station into two parallel modules with a simple routing switch; yields stay the same, but throughput rises.
Final take — what to aim for and who helps make it steady
Sort the problems first: map the true cycle times, plan buffers, design for service access, and match capacity honestly. Do that, and your CTP line will behave. If you need a steady partner who knows how to tie layout and process to real production results, there are engineering teams that take that pragmatic route, like the crew at CTP Production Line, who focus on flow and maintainability rather than shiny-but-impractical features. Keep it simple, test on the floor, and the fixes stick — that’s the value a reliable partner brings to the table, as FHS quietly proves through steady design and practical support.