
Introduction
One hot afternoon in my buddy’s shop, the chatter of chips hitting the tray sounded like a tiny drumline — and that’s where the real talk started. I’ve been watching CNC turn mill center manufacturers sweat over lead times and scrap rates (yeah, they’re gnarly) while data shows shops that adopt smarter workflows cut cycle time by 20–40% — so what gives? This piece drops straight into that scene: scenario, hard numbers, and the question I keep asking my peers — how do we actually make the shop smarter without breaking the bank? I’ll share what I’ve seen, what’s broken, and where I’d place my bets next — stick with me. — moving on to the nuts and bolts.
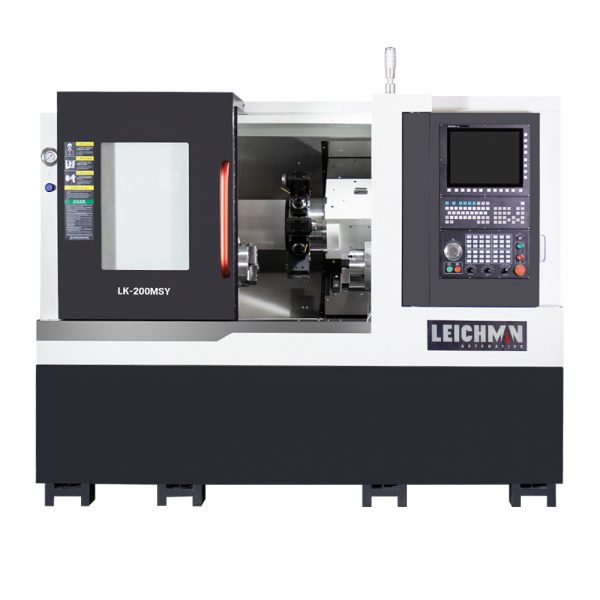
Why Standard Fixes Don’t Cut It for the cnc turning lathe
cnc turning lathe setups are often treated like plug-and-play toys, but trust me — the reality is messier. Old-school upgrades (more horsepower, faster spindles, a slick touchscreen) gloss over systemic problems: inconsistent tool life, poor fixture repeatability, and control software that’s glued to legacy logic. I’ve seen shops crank spindle speed to chase cycle time, only to watch tool wear spike and scrap pile up (ouch). Those quick tweaks rarely touch the deeper issues: bad setup practices, confused job-tracking, and insufficient sensor feedback.
Why does this hurt the bottom line?
Because tight tolerances demand reliable feedback loops. Without decent spindle speed sensors, accurate feed rate adjustments, or a modern CNC controller that can handle adaptive control, you’re flying blind. Add in servo motors that weren’t tuned, linear guideways with play, and tool turret indexing delays — and you’ve got a recipe for variability. Look, it’s simpler than you think: more power doesn’t equal more precision. You need control, diagnostics, and real process insight — not just muscle.
New Technology Principles for the cnc turning and milling center
Here’s where I get hopeful. The next wave isn’t raw speed; it’s principles that stabilize the whole process. I’m talking edge computing nodes that crunch telemetry at the machine, smarter spindle monitoring, closed-loop tool life management, and better human–machine interfaces (HMI) that reduce setup errors. When you combine predictive maintenance data with adaptive feed rate control, you cut surprises — and that’s huge. For anyone investing in a cnc turning and milling center, the payoff is not just faster cycles but fewer resets, less rework, and more predictable throughput.
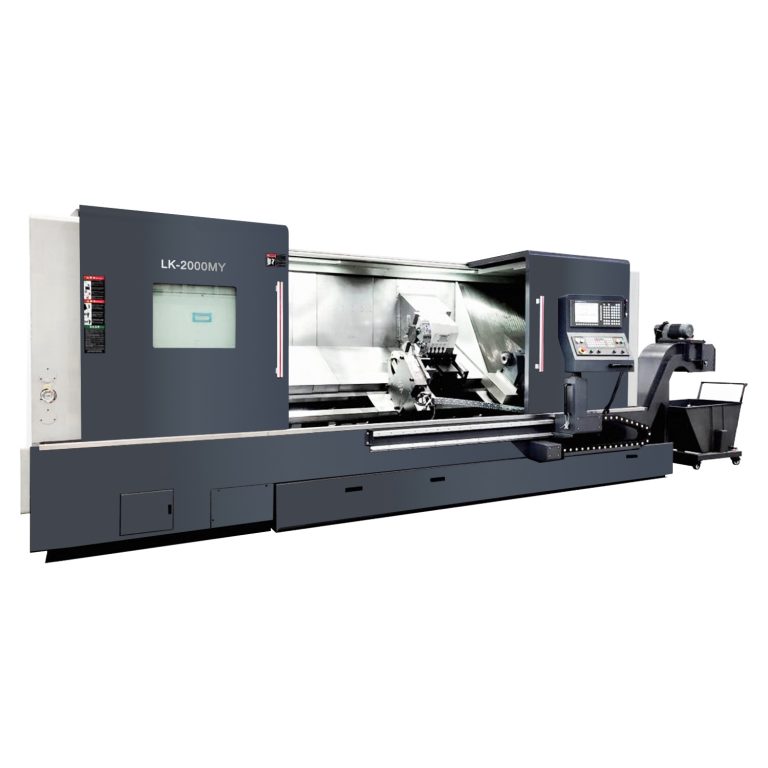
What’s Next — real-world steps?
Start by mapping where variability enters your process: fixtures, tool changes, or CAM post-processor quirks. Then layer in sensors and a minimal edge node to log events (simple — funny how that works, right?). From there, tune your CNC controller for adaptive corrections and shift to data-driven maintenance. I’ve helped teams move from reactive fixes to scheduled, measured improvements; the change is gradual but visible — better OEE, more consistent tolerances, and calmer mornings.
Closing: How I’d Judge New Solutions (3 Quick Metrics)
I’ll leave you with three metrics I actually look at when testing gear or a workflow tweak — they tell you more than flashy specs. First: process variability reduction — measure standard deviation on critical dimensions before and after. Second: setup time delta — track average minutes per job changeover; small savings here compound fast. Third: mean time between adjustments (MTBA) — how long can the machine run without a manual tweak? If a solution improves those, it’s worth the investment. I’m biased, sure — I prefer pragmatic wins over buzzwords — but these measures separate hype from real gain. For anyone who wants a partner in this evolution, I recommend checking out what Leichman offers for modern machining setups: Leichman.