
A Clearer Way to Choose, Not Chase Trends
You’re opening a new store and the timeline is tight. The second call you make is to a shoe cabinet manufacturer after your fit-out lead signs off the layout. You’ve seen this play out: rush orders, mixed finishes, and an invoice that looks fine until the returns start. Last quarter, one buyer told me 18% of shipped units needed rework due to loose hardware, and delivery variance was ±9 days—costly stuff for a seasonal floor set. So here’s the direct question: if the demand is steady and the catalog looks “standard,” why do outcomes vary so much? Is it the spec, the process, or the way we compare suppliers (often apples to oranges)? We tend to compare price and photos. We should compare process stability and fit-for-purpose assembly. That’s where a simple comparative framework helps—materials, tolerances, and assembly design, not just color and knobs. Think no-nonsense, quick checks, and traceable proof. Ready for a clearer view of where the real gaps hide and how to close them? Let’s move from instincts to evidence—one step at a time.
The Hidden Friction in Wholesale Orders
What actually breaks in the process?
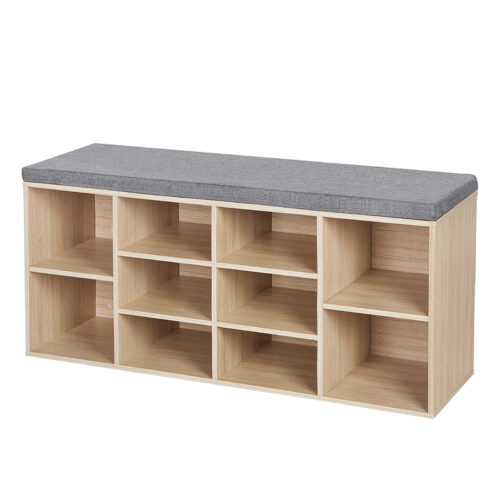
When buying a wholesale shoe cabinet range, the failure points often sit between spec and reality. Panels look right until ABS edge banding lifts after a dry winter. Hinges align during QC but drift once the cam-and-dowel fittings are tightened by store staff. If E1 formaldehyde rating is stated but not validated by batch, a customs check can stall a whole container. Look, it’s simpler than you think: most “quality issues” trace to three things—material stability, hole-pattern tolerances from CNC drilling, and assembly logic under real retail conditions. Traditional fixes focus on thicker board or extra screws. They miss the root cause.
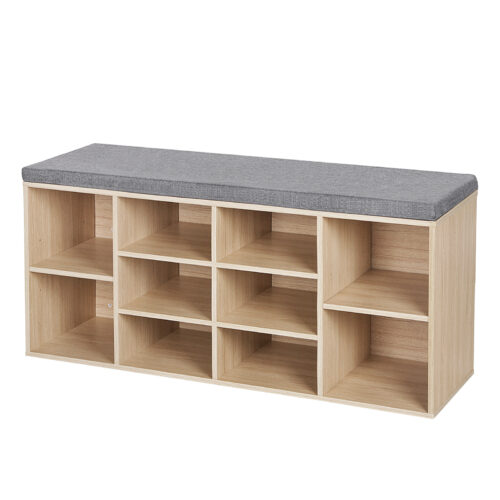
Here’s the technical layer. Low-cost melamine-faced panels with inconsistent density swell unevenly; edge banding then fails under stress—funny how that works, right? Hole drift of ±0.5 mm over long runs seems minor but stacks up across doors, making gaps visible. A powder coating line might improve metal bases, yet if the base-to-case interface lacks a proper pilot, wobble persists. Add SKU sprawl and a high MOQ, and you get complex kitting errors at the warehouse. The pain isn’t only in the product. It’s in the handoff: from CAD to CNC routing, from carton labeling to store assembly SOP. The deeper fix is to spec tolerances, define torque targets, and test for repeatable assembly, not only static load.
Comparative Tech: From Guesswork to Proof
What’s Next
Forward-looking buyers weigh method, not promises. The shift is clear: compare suppliers on process control you can audit. Some shoe cabinet manufacturers in china now run an MES layer that links CNC nesting data to barcode traceability at each station. That means you see which drill bank made the hinge holes, which batch of glue was used on edge banding, and which operator signed off torque on fasteners. It’s not hype; it’s a basic digital thread. Pair that with a short, filmed assembly run using your exact SOP, and you get proof of fit—assembly time, tool list, and a clean pass/fail on door alignment. The principle is simple: control variation at the point of cause; don’t chase it downstream.
Case in point. A retailer swapped two midrange lines that looked identical on paper. Supplier A relied on manual jig checks; Supplier B linked ERP integration to workstation poka-yoke guides and batched panels by humidity band. Over three months, door-gap defects fell from 7.2% to 1.1%. Returns dropped, and install time per unit fell by six minutes—small per unit, big in rollout. The interesting bit is comparative: B did not use exotic materials. They tightened the tolerance window and documented it, then shared batch photos and barcode logs (transparent, calm, Dutch-level practical). That’s the edge—evidence you can reuse across SKUs—and yes, it scales.
If you want a quick, advisory close, use three metrics. First, process capability: require a measured door-gap tolerance and repeatable load-bearing test, tied to batch IDs. Second, assembly reality: request a filmed SOP with torque targets and a timed, two-person build; under 25 minutes signals good design. Third, stability signals: look for ISO 9001 plus a simple MES report that traces CNC drilling and edge banding to operator and shift. Evaluate those three, and price talks make sense. Keep it steady, compare like for like, and you’ll avoid the usual surprises. For a grounded reference point in this space, see SONGMICS HOME B2B.