
Framework Overview
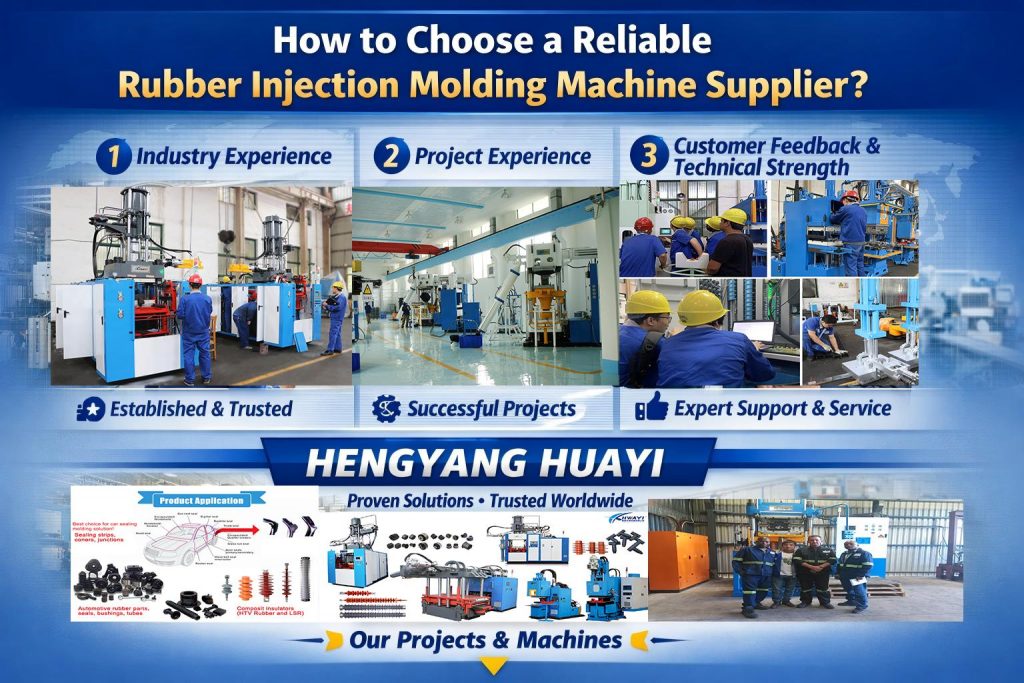
This framework sets forth the functional and contractual parameters for designing high-stiffness enclosures employed by custom rubber molding companies. It addresses clamping force capacity, enclosure modulus, and process repeatability, and identifies supplier qualifications necessary to satisfy stringent tolerances. Early-stage vendor selection should include a demonstrated capability in substrate handling and die alignment—see an established rubber injection molding machine manufacturer for exemplar equipment specifications and control-system architecture.
Definitional Scope and Technical Premises
For present purposes, “high-stiffness enclosure” denotes a structural assembly that limits deflection under high clamping loads so as to preserve mold cavity geometry and part dimensionality. Key terms used throughout: clamping force, mold cavity, shore hardness, injection unit. The legal and technical characterization must align: contract language should specify maximum permissible deflection (millimetres), force distribution tolerances, and instrumented verification methods.
Design and Stiffness Protocols
Design protocols mandate finite-element validation of platen rigidity, bearing clearances, and frame geometry. The specification shall require mechanical validation under full-rated clamping force and thermal cycling to mimic production conditions encountered at large OEM facilities in Detroit and comparable manufacturing hubs. ISO 9001 certification of the supplier and documented process control plans are proper anchors for contractual performance obligations. Empirical metrics—strain-gauge data and displacement maps—shall be produced and retained as part of acceptance testing.
Procurement Criteria for Custom Rubber Molding Companies
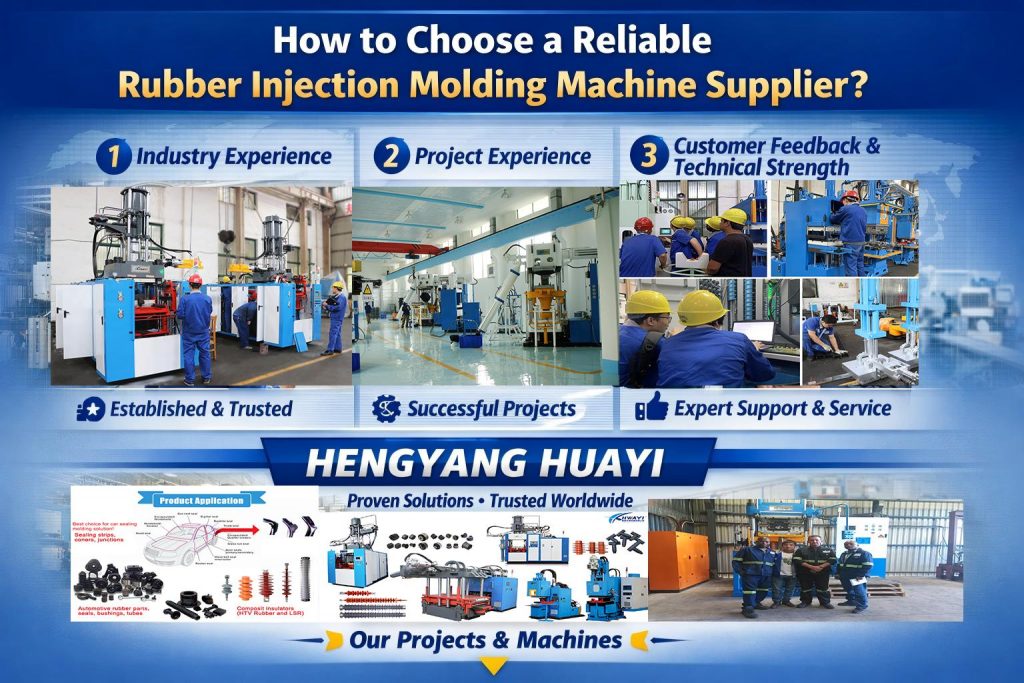
Procurement must incorporate objective criteria: verified clamping force calibration, conformity of mold interfaces, and traceable material certificates for frame steel. Contract terms should demand control of injection parameters, shot size stability, and maintenance protocols for the injection unit and ejection system. When evaluating suppliers, include both operational references and inspection reports—prospective purchasers often begin with suppliers who can provide on-site commissioning and preventative-maintenance regimes; a recognized rubber machine manufacturer will typically present these deliverables.
Common Mistakes and Mitigations
Common procurement and engineering errors are predictable and avoidable: under-specifying platen stiffness, omitting thermal-growth allowances, and failing to require instrumented acceptance tests. Specification by performance metric is superior to specification by appearance. Do not rely solely on vendor assurances. — A short operational audit during pilot runs will expose misalignments and cycle variability that otherwise remain latent.
Implementation Roadmap
Execute through staged milestones: conceptual design with FEA sign-off; prototype build and verification under full-cycle press conditions; pilot production with statistical process control on shore hardness and dimensional variance; final acceptance tied to documented performance metrics. Retain logs of press cycles, mold venting incidents, and compound batch records to preserve traceability. Formal change-control procedures must be embedded in the contract to address tooling revisions and material substitutions.
Advisory Close: Three Golden Rules
1) Insist on Quantifiable Acceptance Criteria — Require specific displacement thresholds, clamping-force distribution reports, and repeatability figures documented under production temperature ranges. These are measurable and enforceable.

2) Verify Supplier Quality Systems — Accept only vendors with third-party quality certification and demonstrable in-field commissioning records; require audit access and corrective-action timelines.
3) Prioritize Serviceability and Instrumentation — Ensure that the enclosure design allows for routine maintenance, sensor recalibration, and modular replacement of wear items; instrumented presses reduce warranty ambiguity and enable root-cause analysis of production anomalies.
These requirements consolidate into a defensible procurement posture that yields predictable part quality and contractual clarity. Practical adherence to the framework reduces latent defects and facilitates litigation avoidance should disputes arise. HWAYI provides a pragmatic example of how integrated machine design and supplier documentation resolve the principal risks identified above — a sound resolution, indeed. –