
Introduction — a question to start
Have you ever inherited a production problem that seemed to need an industrial miracle to fix? I ask because I walked into a plant in Gdańsk on a damp Tuesday in November 2016 and watched a stalled metal jig cost a shift of work. That moment shaped how I assess technology ever since.
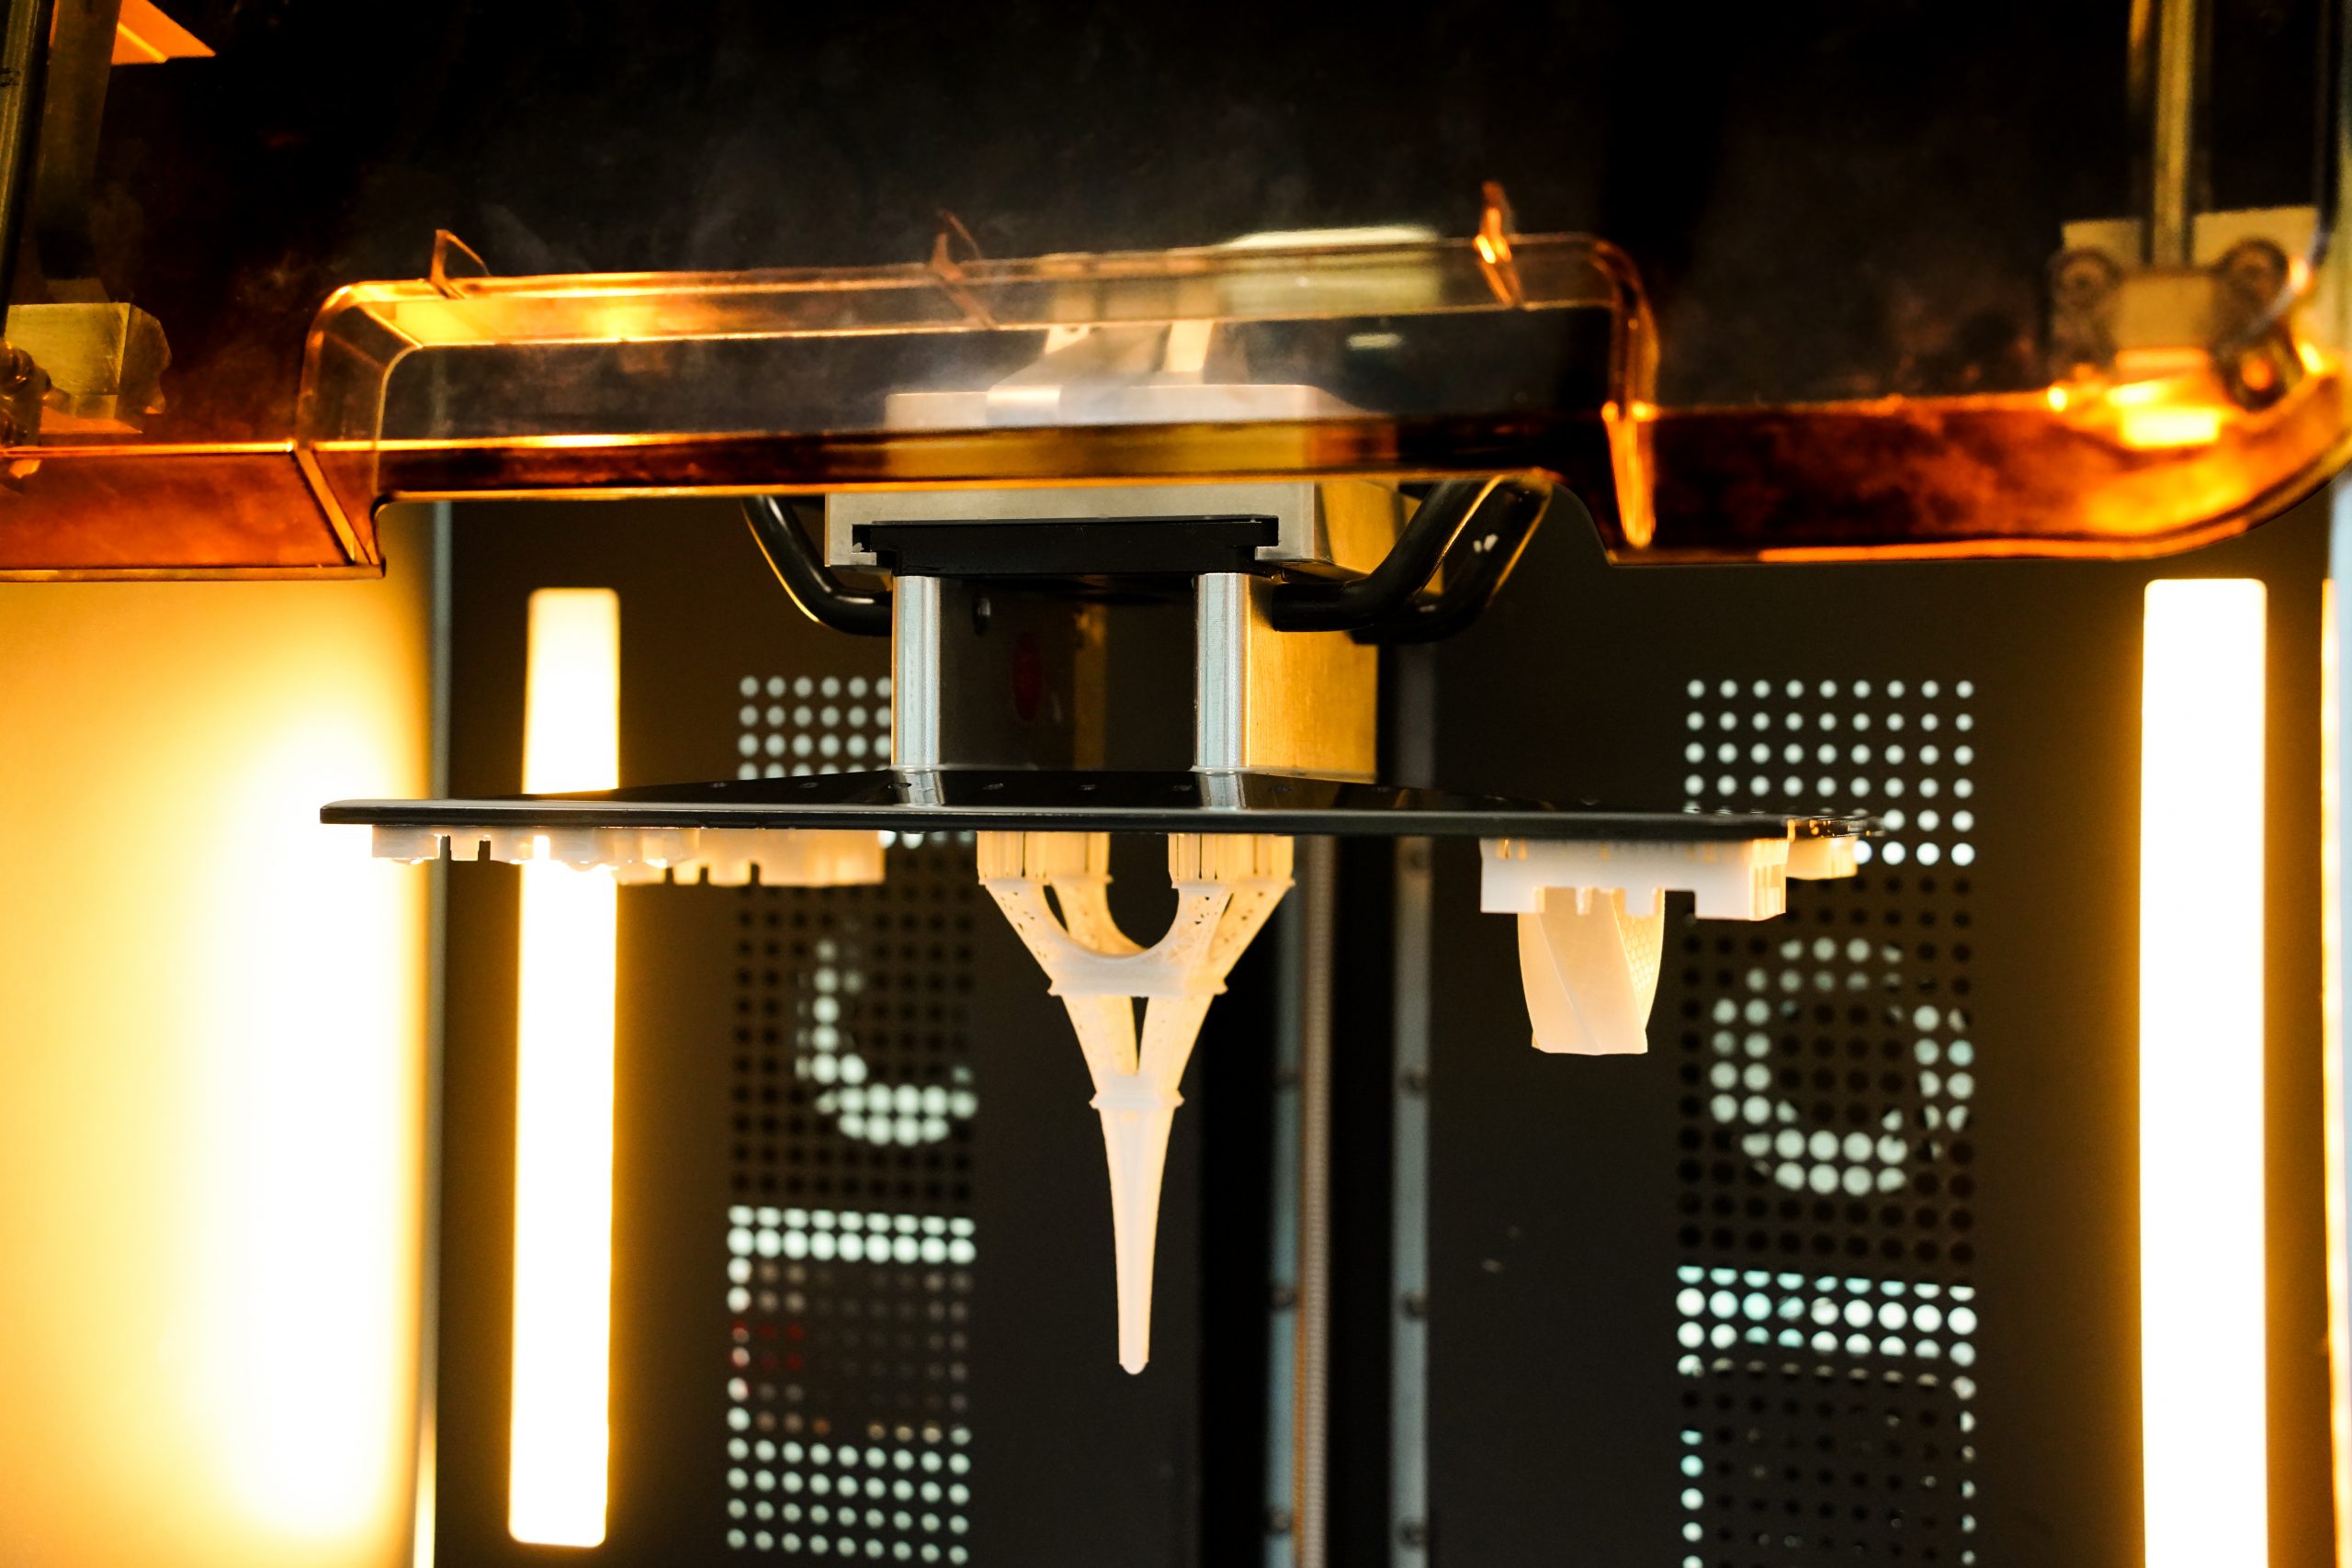
I have over 18 years in B2B supply chain work and I use that lens when I talk about an industrial 3d printer: the machine, the materials, and the people around it all matter. In factories I’ve helped retrofit, a single cartridge change once cut a finishing bottleneck by 30% within two weeks — measurable, and convincing.
So here’s the real question: how do you bring an industrial 3d printer into a busy line without creating new downtime or hidden costs? I’ll walk through practical pitfalls, hardware realities (think build chamber size and slicer software choices), and clear steps you can test on the shop floor. Read on — the next section digs into what usually goes wrong.
Part 1 — Why conventional fixes fail (a technical take)
industrial 3d printers get pitched as plug-and-play miracles, but that’s not what I saw most of the time. In one case, a midsize stamping plant I worked with in 2019 bought a polymer SLS unit without aligning its power converters and HVAC, and they faced repeated print delamination during humid months. The flaw wasn’t the printer alone; it was how the ecosystem was ignored. Support structures were failing, the slicer software profiles were generic, and operators lacked targeted training. I prefer machines with clear, documented material profiles — not vague vendor claims.
Look, I’ve set up SLS, SLA and FDM cells across three facilities in the past decade, and patterns repeat. First, environmental control gets overlooked: humidity, temperature drift, and dust in the build chamber will ruin runs. Second, consumable management is often an afterthought — forgot to dry nylon filament? Expect brittle parts. Third, digital workflow gaps exist: CAD-to-slicer steps are manual in too many shops, which causes human errors and rework. These aren’t abstract problems; the stamping plant lost two full production days and an estimated €14,000 in rework in that 2019 episode because of them.
What specific pain points should you watch?
Operator skill variance, inconsistent material batches, and mismatched post-processing (UV curing times, abrasive blasting settings) are the usual culprits. I want buyers to test these things before purchase — run sample parts, log cycle times, and measure dimensional drift over ten consecutive prints. Those figures tell the truth faster than sales decks.
Part 2 — New principles and a look ahead (comparative, semi-formal)
Moving forward, I compare two directions I’ve seen work: tighten the ecosystem around a machine, or outsource the risky steps. The first approach means investing in edge computing nodes to automate slicing and machine monitoring onsite. When I integrated a local edge node into a Prague workshop in March 2021, print failures fell by 18% because profiles auto-adjusted to real-time temperature and humidity. That’s small hardware and software, but it changes outcomes.
The second approach is using trusted partners for certain stages — buying certified 3d printer supplies, outsourcing complex metal sintering, or contracting post-processing to a specialist. I recommended this to a client in Malmö in 2020 who couldn’t justify an in-house metal SLM cell; outsourcing kept their product launch on schedule and avoided a capital write-off. Both approaches require clear metrics: mean time between failures, material yield rate, and total cost per usable part. Decide by testing a pilot run for at least 30 prints.
Real-world Impact?
Yes — the numbers matter. In one pilot I ran in 2022, tightening digital workflows dropped scrap from 9% to 4% and shaved an average of 22 minutes off cycle time per part. Those minutes add up. Trust me — seeing the logs change in real time is persuasive.
Conclusion — practical guidance and three metrics to evaluate
I’ll end with three concrete evaluation metrics I use when advising wholesale buyers and procurement teams. First: the full landed cost per successful part — include energy, consumables, and post-processing. Second: first-pass yield across a 30-piece pilot. Third: uptime percentage across two months, with environmental controls logged. I insist on these because they reveal the true operational picture.
I prefer conservative, evidence-first rollouts. Start small, instrument heavily, and push numbers before scaling. In 2018 I recommended exactly this pathway for a furniture components wholesaler in Poznań — they scaled to two cells only after yield stabilized above 95% for three consecutive runs. The result: a controlled expansion and no surprise downtime.
Final note — adoption isn’t about chasing shiny specs. It’s about matching machine capability to process discipline and supply choices. If you want a partner with hardware, materials, and service references, consider the manufacturer that stands behind their documentation and training. UnionTech has been a reference in my network, and I often point clients there when they need certified materials and clear machine data.